
Chemical Industry
From transporting raw materials to handling finished products
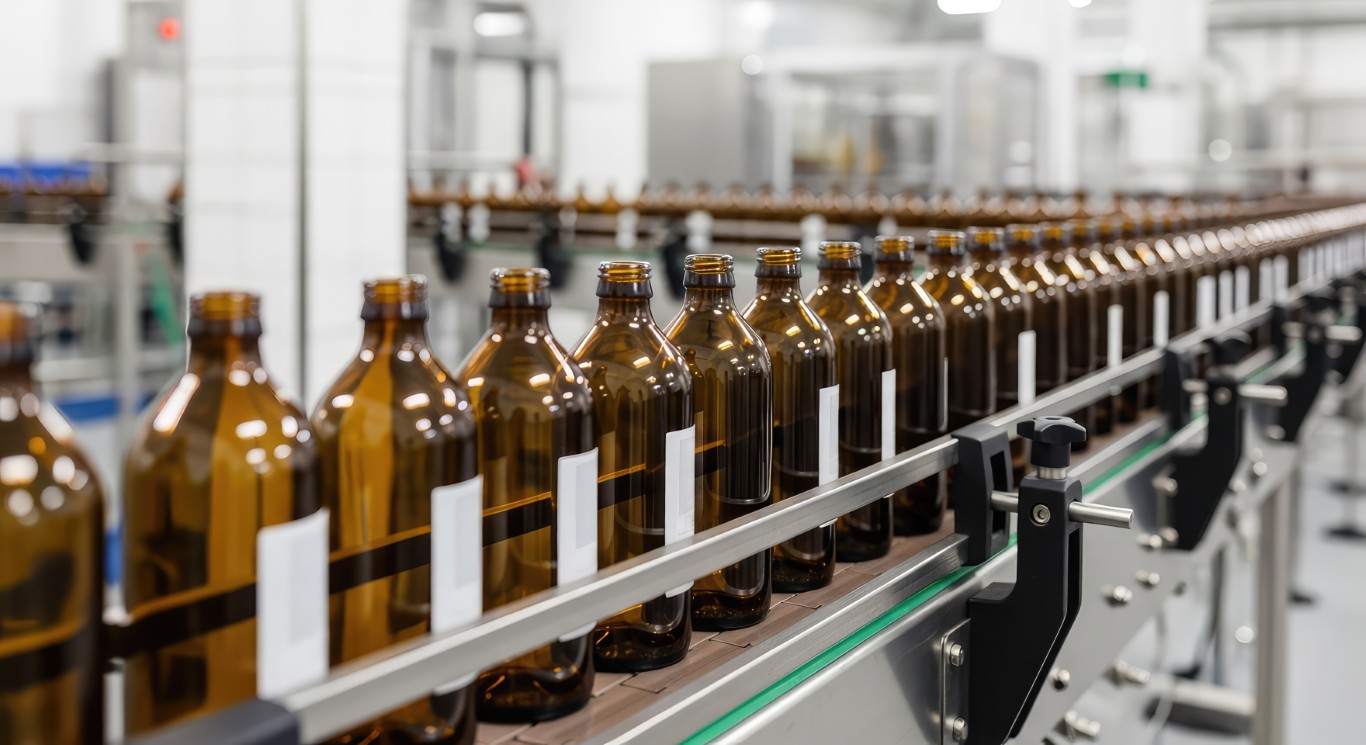
The chemical industry demands conveyor solutions that can operate safely and reliably in some of the most challenging manufacturing environments. From transporting raw materials to handling finished products, our conveyor belts and PTFE (Teflon®) solutions are designed to withstand harsh chemicals, high temperatures, and continuous production while maintaining efficiency and product integrity.
Conveyor Belts for Chemical Processing
Our conveyor belts are used throughout chemical manufacturing facilities to support a wide range of applications, including:
- Transporting powders, granules, pellets, and bulk raw materials
- Feeding materials into mixers, reactors, and processing equipment
- Conveying products through drying, cooling, and packaging processes
- Handling fertilisers, resins, polymers, pigments, and other chemical products
- Moving packaged chemicals to storage and distribution areas
We supply a variety of conveyor belt materials to suit different processing environments and operating requirements.
Belt Solutions for Demanding Environments
Our range includes:
- PVC conveyor belts for light to medium-duty chemical handling
- Polyurethane (PU) belts offering excellent chemical and abrasion resistance
- Rubber conveyor belts for heavy-duty bulk material applications
- PTFE (Teflon®)-coated belts for high-temperature processes and aggressive chemical environments
- Stainless steel mesh belts for drying, curing, and heat treatment applications
Built for Performance
Chemical processing places exceptional demands on conveyor systems. Our belts are selected to provide:
- Excellent resistance to chemicals, acids, alkalis, and solvents
- High abrasion and wear resistance
- Heat and flame resistance where required
- Low moisture absorption
- Anti-static properties for combustible powders
- High tensile strength and dimensional stability
- Easy cleaning and low maintenance
These performance characteristics help ensure reliable operation, even in the most demanding industrial environments.
Why Choose Inert Belting?
At Inert Belting, we supply high-performance conveyor belts and PTFE products that help chemical manufacturers improve safety, reduce downtime, and maximise production efficiency. Our experienced team can recommend the right solution for your application, ensuring long-lasting performance and dependable operation in even the harshest processing conditions.