
Pharmaceutical Belting
Belting plays a critical role in pharmaceutical manufacturing
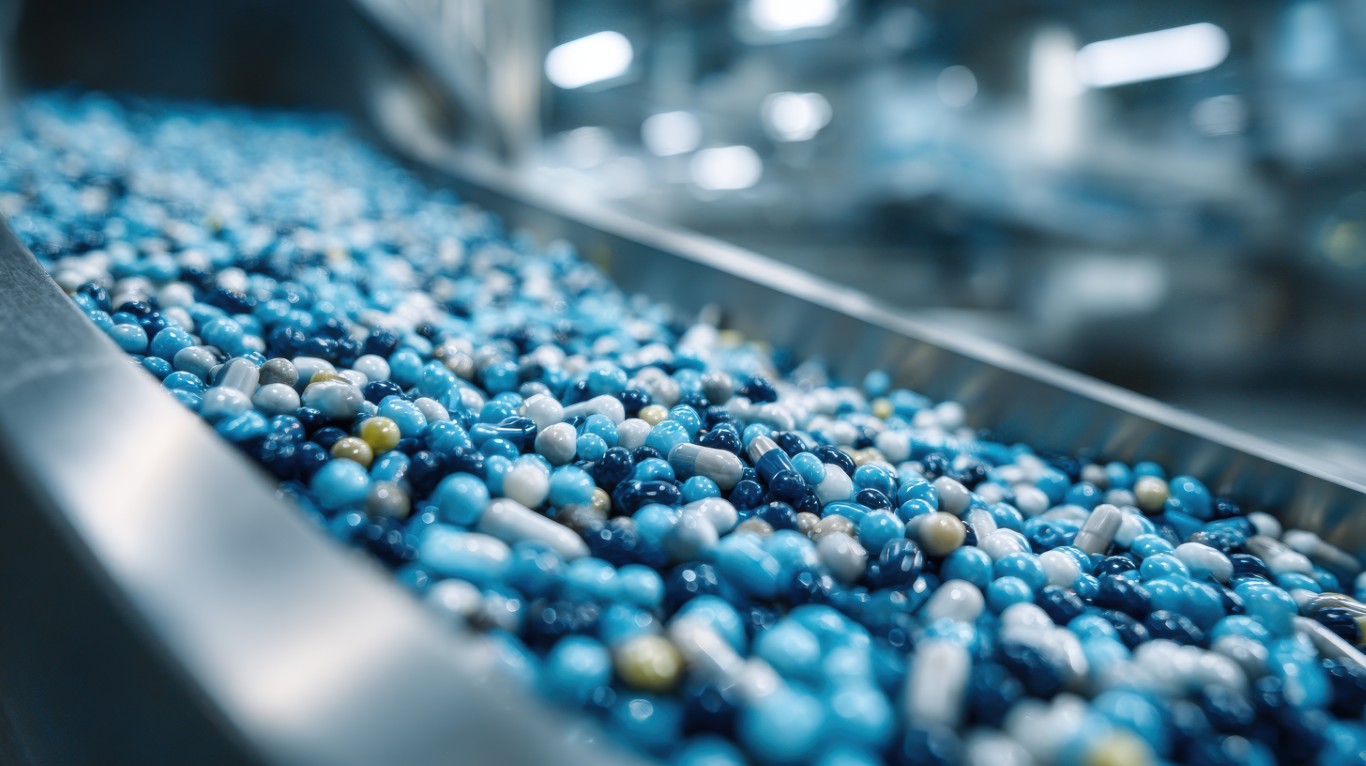
The pharmaceutical industry requires conveyor systems that deliver exceptional levels of hygiene, precision, and reliability. From handling raw ingredients to packaging finished medicines, our conveyor belts are designed to support efficient production while helping manufacturers meet strict quality and regulatory standards.
Conveyor Belts for Pharmaceutical Manufacturing
Our conveyor belts are used throughout pharmaceutical production facilities to ensure the safe and efficient movement of products at every stage of the manufacturing process, including:
- Transporting powders, granules, and raw ingredients to processing equipment
- Moving tablets and capsules through granulation, compression, coating, and inspection
- Conveying bottles, blister packs, cartons, and labels through filling and packaging lines
- Supporting visual inspection, metal detection, and quality control systems
- Operating in cleanroom and sterile production environments where contamination must be minimised
We supply a comprehensive range of belting solutions designed to meet the demanding requirements of pharmaceutical manufacturing.
Belt Solutions for Hygienic Production
Our range includes:
- Polyurethane (PU) conveyor belts for hygienic, pharmaceutical-grade applications
- PVC conveyor belts for light-duty conveying and packaging operations
- Modular plastic belts for durable, low-maintenance washdown environments
- Timing belts for precise synchronisation in automated machinery
- Round and flat belts for power transmission in pharmaceutical equipment
Designed for Clean, Reliable Performance
Our conveyor belts are selected to deliver the performance required in highly regulated manufacturing environments, offering:
- Hygienic, non-toxic materials
- Smooth, non-porous surfaces for easy cleaning
- Excellent resistance to cleaning agents and process chemicals
- Low particle generation
- High wear and abrasion resistance
- Anti-static properties where required
- Compliance with pharmaceutical and food-contact standards where applicable
These features help manufacturers maintain product integrity, reduce downtime, and support efficient, continuous production.
Why Choose Inert Belting?
At Inert Belting, we understand the importance of hygiene, accuracy, and reliability in pharmaceutical manufacturing. Our experienced team can recommend the ideal conveyor belt for your production process, helping you improve efficiency while supporting compliance with the industry’s strict quality and regulatory requirements.
Whether you’re manufacturing tablets, capsules, powders, liquids, or packaged pharmaceutical products, we provide high-performance belting solutions designed to keep your production moving safely and efficiently.